Case:
Background & Challenge
A leading manufacturer of hygiene products planned to relocate its production facility to a larger site with significantly increased production capacity. As part of the expansion, the customer wanted to reduce the footprint of its filtration systems while lowering maintenance requirements and minimizing production downtime.
The existing setup consisted of one dedicated filtration system per production line, utilizing a combination of drum filters and baghouse filters. With eight production lines operating at a total airflow of 360,000 m³/h, the system occupied substantial floor space and required extensive spare parts inventory and maintenance resources.
PF System’s Solution
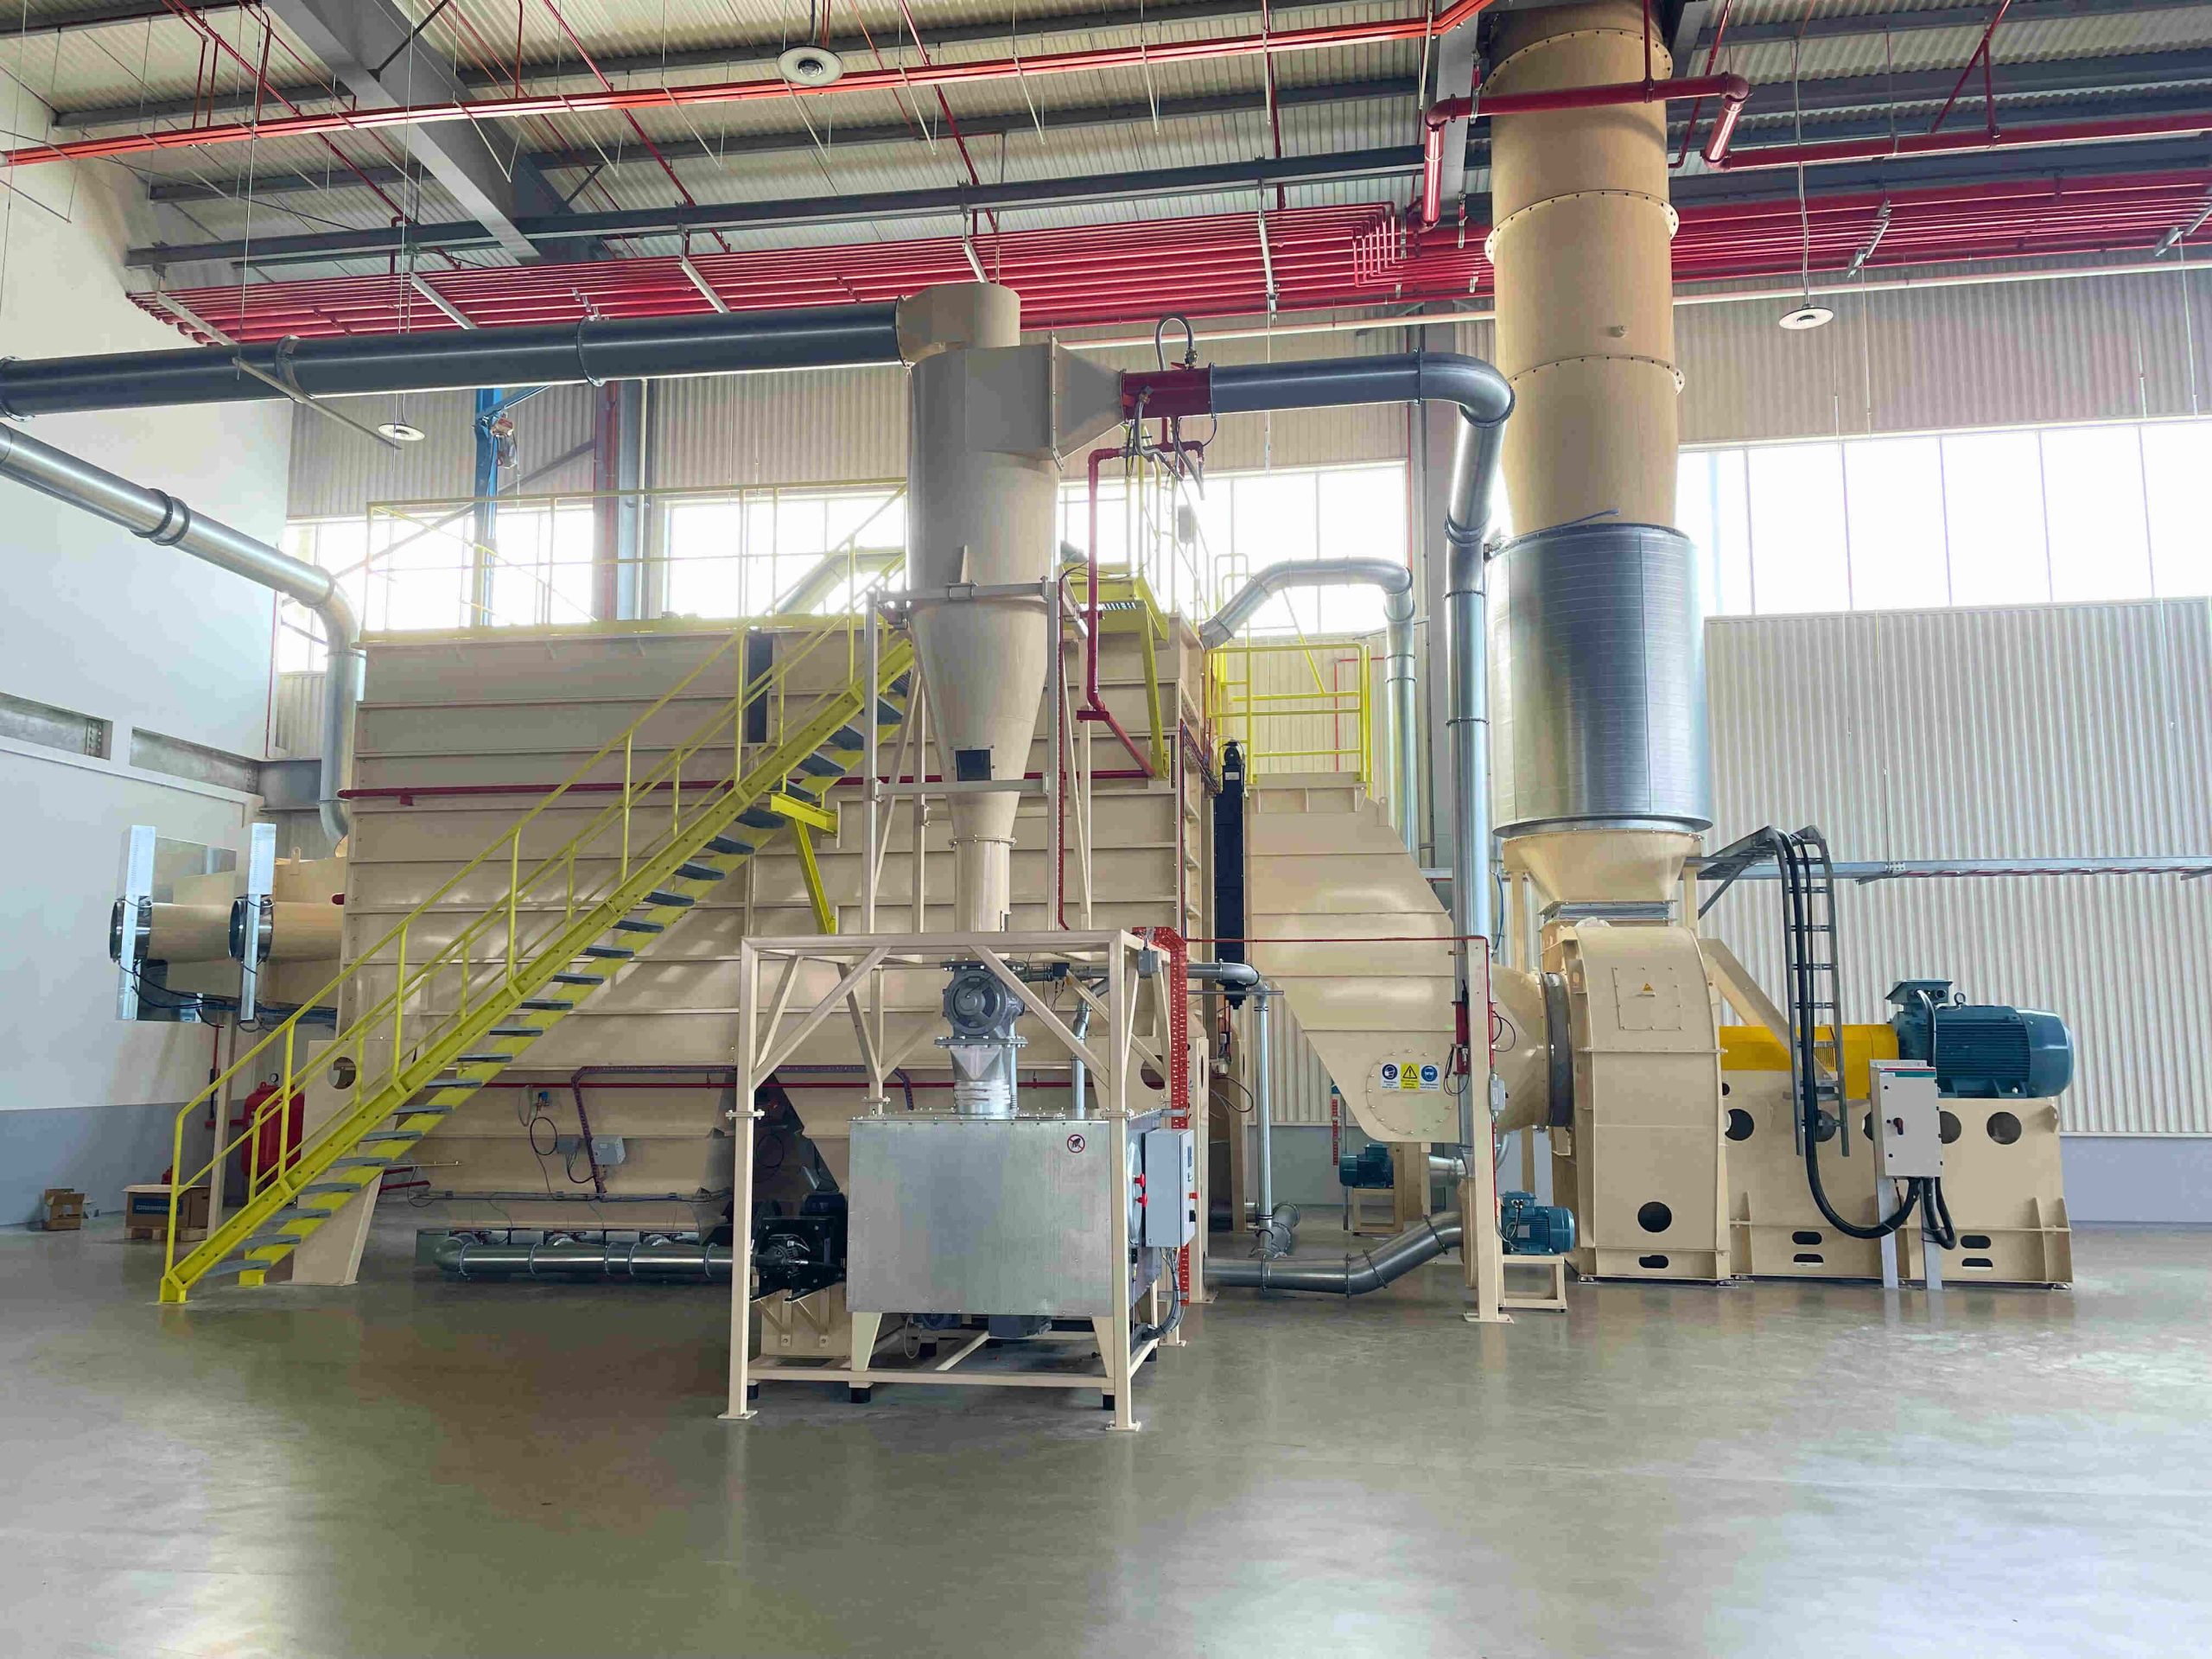
PF System evaluated the production process and developed a centralized multi-line filtration concept based on PF System’s CCF filtration units.
Instead of allocating one filter system to each production line, multiple production lines were connected to larger filtration units with capacities ranging from 60,000 to 130,000 m³/h. This approach significantly reduced the number of filtration units required while maintaining high process reliability and flexibility.
The system automatically adjusts airflow according to the number of active production lines, ensuring optimal energy efficiency and process performance at all times. The CCF filtration technology was also designed to handle very high dust loads, including demanding applications involving fine Super Absorbent materials.
Results
Customer Value
The filtration units were manufactured and shipped from Sweden and installed at the customer’s facility in Asia together with the customer’s experienced installation partner. Final commissioning was performed by PF System specialists to ensure optimal system performance from day one.
Comprehensive operator training enabled the customer’s maintenance and production teams to independently manage daily operation of the filtration system. In addition, PF System’s remote support service, integrated through the electrical control cabinet, provides ongoing access to expert assistance whenever required.
By implementing a centralized multi-line filtration solution, the customer achieved a highly reliable, cost-effective, and future-proof system that combines reduced operating costs, simplified maintenance, and exceptional process flexibility for high-capacity hygiene product manufacturing.